
From Boiler Feed to Desulfurization, Shakti Pumps Showcases Solutions for the Complete Boiler Water Journey at Boiler India 2026

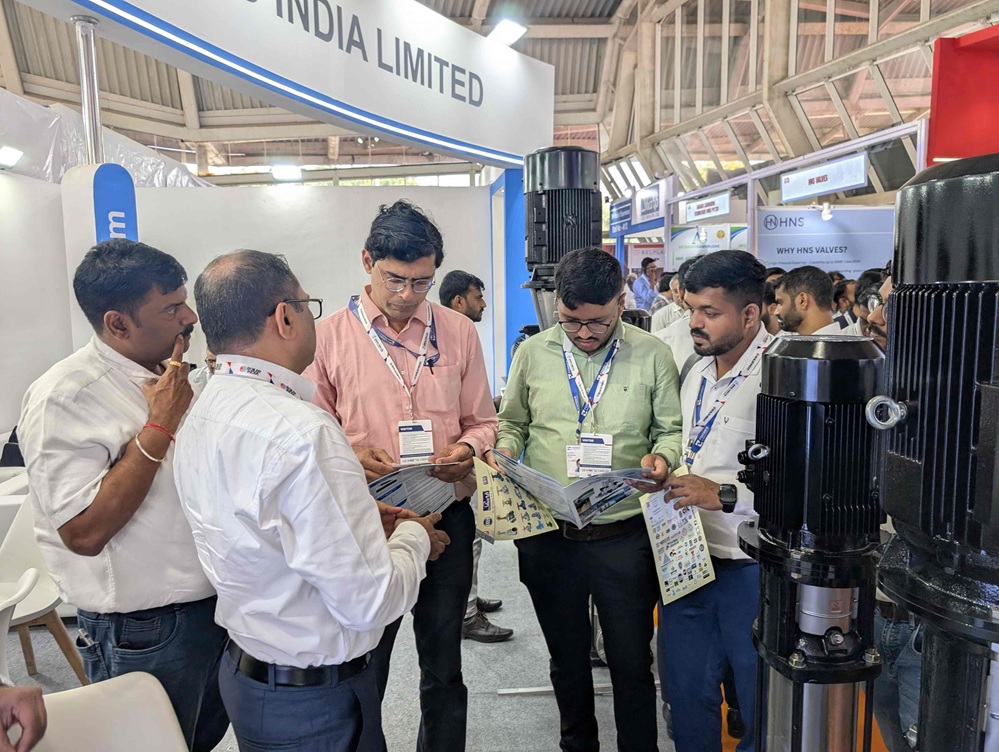
Navi Mumbai : Shakti Pumps (India) Limited, a leading manufacturer of energy-efficient pumping solutions, is showcasing its integrated industrial pump portfolio at Boiler India 2026, being held from October 8–10 at the CIDCO Exhibition & Convention Centre, Navi Mumbai.
Through its participation at Boiler India 2026, Shakti Pumps is highlighting its growing capabilities in specialised industrial pumping applications, bringing together solutions designed to support the complete water journey within boiler systems, from feedwater and condensate management to emissions-control applications. The company thus offers purpose-built pumping solutions engineered for the specific requirements of each stage.
Mr. Ramesh Patidar, Managing Director, Shakti Pumps (India) Limited, said, “Industrial boiler systems demand pumping solutions that can deliver reliable performance across multiple critical stages from high-pressure boiler feed and condensate recovery to desulfurization applications. Our approach is to look at the complete water journey within the system and engineer solutions around the specific duty and operating environment. Through our expanding industrial portfolio, we are bringing together energy-efficient and application-specific technologies designed to support reliability, ease of maintenance and lifecycle performance.”
A key highlight is Shakti Pumps’ SCR, SCRI and SCRN vertical multistage centrifugal pump range, engineered for the high-head, high-temperature and high-pressure requirements of boiler feed lines and also suited to desulfurization and wet-scrubber circuits. The range can deliver heads of up to 322 metres and flows of up to 180 m³/hr, with motor options from 0.5 HP to 100 HP.
The pumps feature sheet-metal fabricated construction, balanced impellers and couplings, cartridge mechanical seals, vibration-absorbing components, H-class insulation and laser-welded components, with IE3, IE4 and IE5 motor options available for applicable requirements. These features are designed to support smooth, reliable operation and ease of servicing in demanding boiler environments.
The range is available in different material configurations, with SCRI in SS304 and SCRN in SS316. SS316 provides greater resistance to chlorides and aggressive process water, making it suited to more demanding applications such as desulfurization and wet-scrubber circuits, while SS304 is positioned for standard boiler feed duty.
For condensate recirculation, Shakti Pumps is showcasing its Monoblock pump range, in which the impeller is mounted directly on the extended motor shaft. This integrated configuration eliminates the need for a separate coupling and shaft alignment, offering a compact solution for condensate return systems.
The Monoblock range comes with IE3 motors as standard, with IE4 and IE5 options, alongside sheet-metal fabricated impellers, laser-welded construction and H-class insulation.
For desulfurization and wet-scrubber applications, suitable SCR, SCRI, SCRN and Monoblock configurations are available, including SS316 options for corrosive-duty applications and nano and ceramic coating options for relevant requirements.
Across its boiler portfolio, Shakti Pumps is also focusing on serviceability and operating performance, with features such as cartridge mechanical seals, duplex steel shafts, tungsten carbide bearings and vibration-absorbing components designed to support durability in continuous-duty applications. The company also offers its S4RM motor technology, designed to deliver energy-saving benefits without requiring additional VFD equipment in suitable applications.
The portfolio therefore maps directly across the boiler water cycle: SCR/SCRI/SCRN pumps for boiler feed, Monoblock pumps for condensate recirculation, and suitable configurations for desulfurization and wet-scrubber systems.
